Surface Grinding Wheels

Surface Grinder Grinding Wheels
Peripheral grinding:
End face grinding:
Peripheral & end face grinding
The surface grinding process system has good rigidity, can adopt a larger grinding amount, has a very high grinding efficiency, and has high workpiece processing quality.

Surface grinding is a kind of technology which is used for precision grinding of flat workpiece. It is used for grinding planes, grooves of the workpiece on the surface grinder by the traditional grinding wheels or diamond grinding wheels or CBN surface grinding wheels.
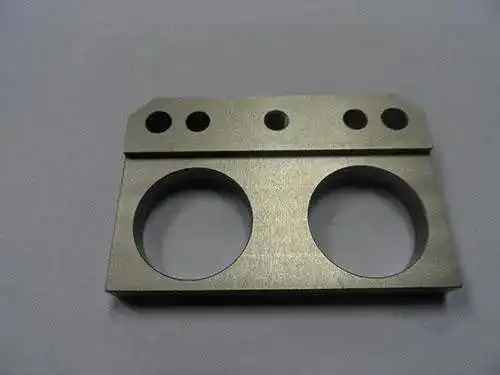
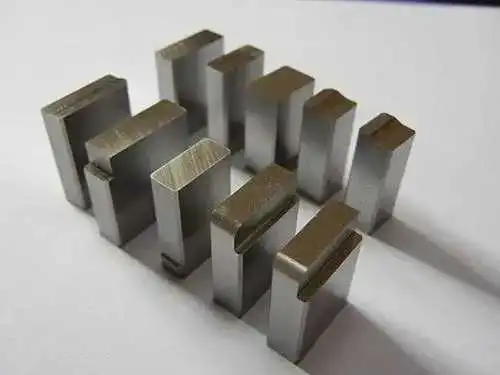
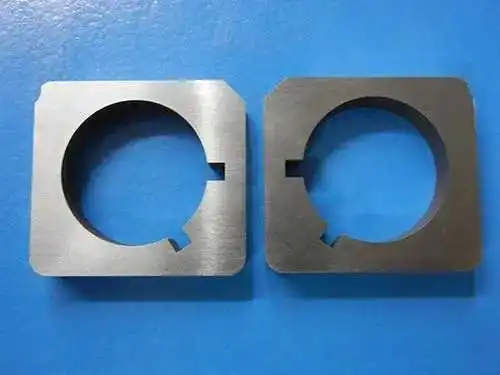
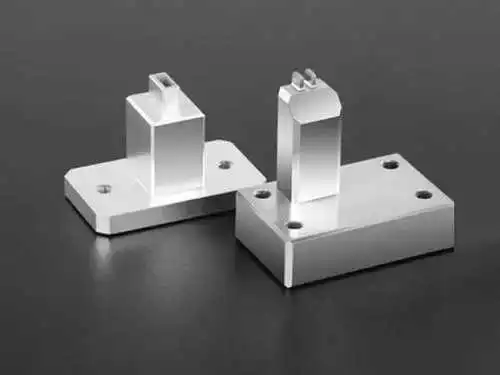
surface Grinding Workpiece Display
Surface Grinding Wheels types:
According to the different working surface of grinding wheel, surface grinding can be divided into three methods: peripheral grinding, end face grinding, and peripheral end face grinding.
Peripheral Grinding:

also known as circumferential grinding, is to use the circumferential surface of the grinding wheel for grinding. Surface grinder with horizontal axis belongs to this form.
Features of Peripheral Grinding
It can reduce the deformation of the workpiece caused by heating, which is good for improving the grinding accuracy of the workpiece. It is suitable for precision grinding of various workpieces, the flatness error can be controlled within 0.01-0.02mm/1000mm, and the surface roughness can reach Ra0.8-0.2μm.

However, due to the need for intermittent lateral feed to complete the grinding of the workpiece surface without grinding, the production efficiency is low.
Because of small depth of cut and long reciprocating time of the worktable, the production efficiency is relatively low.
End Face Grinding:
grinding with end face of the grinding wheel. Surface grinder with vertical axis belongs to this form.
Features of End Face Grinding
Choose the larger grinding amount when the bending deformation is small and the rigidity is good.

The production efficiency is high, and the workpieces are prone to thermal deformation and burn, and the end face grinding is suitable for workpieces with low grinding accuracy and simple shapes. To improve the quality of end face grinding, the following measures can be taken.
① Select resin bond grinding wheels with coarser grain size and softer hardness.
② Provide sufficient cutting fluid when grinding.
③ Grinding with segmented wheel.
④Dress the end face of the grinding wheel into an inner cone shape, making the grinding wheel and the workpiece are in linear contact or adjusting the angle, reducing the contact between the grinding wheel and the workpiece and improving the heat dissipation conditions.
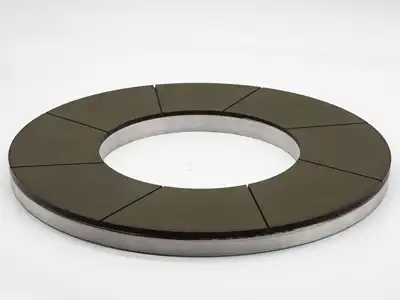
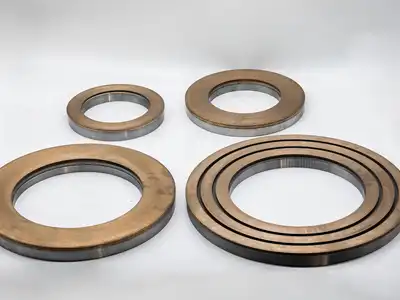
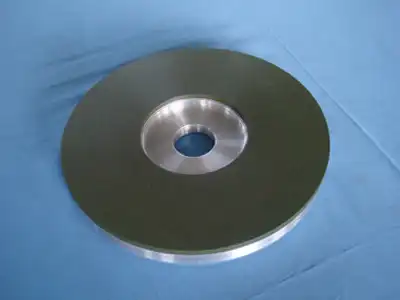
Peripheral & End Face Grinding:
Grinding the circumference and end face of the grinding wheel at the same time. When grinding the step surface, if the step is not deep, use the grinding wheel with peripheral & end grinding on the horizontal axis and rectangular table surface grinder.
Features of peripheral-end face grinding: The grinding amount should not be too large.
Methods of Surface Grinding
Transverse Grinding Method
When transverse grinding, the longitudinal stroke of the worktable is completed, the grinding wheel shaft or worktable makes transverse feed. At this time, the thickness of metal layer ground by the grinding wheel is the actual depth of cut.
After the first layer of metal on the workpiece is ground, the grinding wheel makes a vertical feed again, and the grinding heat changes the direction to continue to make transverse feed. The second layer of metal allowance on the workpiece is ground, and repeat this process of grinding multiple times until all the allowance is removed.

The transverse grinding method is suitable for grinding long and wide surface. Because of the small grinding contact area, good debris removal and cooling condition, the surface grinding wheel is not easily blocked, the grinding heat is small, and the workpiece deformation is small, ensuring the machining quality of the workpiece. But the production efficiency is low, and the grinding wheel wear is uneven. When grinding, pay attention to the grinding amount and the selection of the grinding wheel.
Deep Grinding Method
When grinding, the grinding wheel only makes two vertical feeds. The first vertical feed rate is equal to the total allowance of rough grinding.

When the longitudinal stroke of the worktable ends, move the grinding wheel or workpiece along the grinding wheel axis direction by 3/4 to 4/5 of the grinding wheel width until all the rough grinding allowance of the workpiece is cut off.The second vertical feed rate is equal to the precision grinding allowance, and the grinding process is the same as that of the transverse grinding method.
The feature of deep grinding method is high production efficiency, and it is suitable for mass production or large-scale grinding. During grinding, pay attention to the sufficient cutting fluid for cooling.
Step Grinding Method
Depending on the size of the grinding allowance of the workpiece, dress the grinding wheel into a stepped shape, grinding off the entire surface allowance by the smaller transverse feed rate in one vertical feed.
When step grinding , due to the large grinding amount, the transverse feed should be slowe in order to ensure the quality of the workpiece and improve the life of the grinding wheel. The step grinding method has high production efficiency, but it is more difficult to dress the wheel, and the machine tool should have high stiffness, so it is limited in application.

Selection of Surface Grinding Wheels
Based on the grinding method, workpiece material, processing requirements, and ect, choose the surface grinding wheel. The plane grinding wheel is usually used for peripheral grinding. The cylindrical grinding wheel is usually used for end face grinding.


Diamond grinding wheel is mainly used for grinding cast iron, tungsten carbide, and engineering ceramics, etc.. CBN grinding wheel is used for grinding materials containing iron group elements, such as stainless steel, tool steel, high-speed steel, etc
Performance comparison of diamond grinding wheels with various binders
Type of Binder | Self-Sharpening | Sharpness | Life | Dressing Difficulty | Price |
Metal | 3/5 | 3/5 | 3/5 | 5/5 | 4/5 |
Resin | 5/5 | 4.5/5 | 3/5 | 1/5 | 2.5/5 |
Vitrified | 5/5 | 5/5 | 4/5 | 1/5 | 4/5 |
Electroplated | 4.5/5 | 5/5 | 3/5 | 0.5/5 | 4/5 |
Metal-Resin | 4/5 | 4.5/5 | 5/5 | 3/5 | 5/5 |
Related Products


INQUIRY
Please Feel free to give your inquiry in the form below. We will reply you in 24 hours.