External cylindrical Grinding Wheels

External Cylindrical Grinding
- Longitudinal Grinding Method
- Cutting-in Grinding Method
- Segmented Grinding Method
- Deep Grinding Method
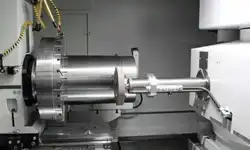
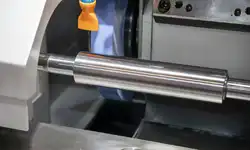
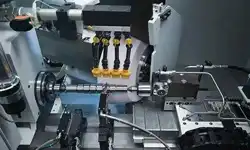
External cylindrical grinding wheel is mainly used for grinding the outer cylinder, outer cone and shoulder end face of shaft workpieces.
External cylindrical grinder is mainly used for precision grinding of end face, outer cylinder, and conical surface of batch shaft parts, and it is main equipment in automotive engine industry.
It is also suitable for processing shaft parts with high precision requirements in the military, aerospace, and medical industries. External cylindrical grinding wheel can process various types of materials, including metals such as steel, aluminum, and titanium alloys, as well as tungsten carbide, ceramics, and composite materials.
External Cylindrical Grinding Workpiece Display
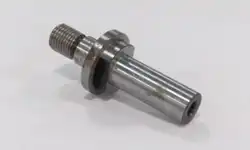
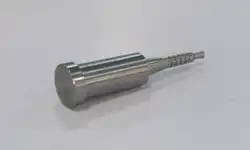
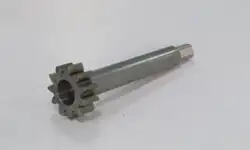
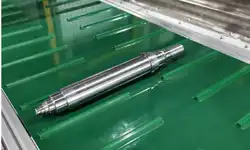
Methods of External Cylindrical Grinding :
There are 4 types of cylindrical grinding methods including longitudinal grinding, cutting-in grinding, segmented grinding, and deep grinding. The method can be selected based on the shape, size, machining allowance, and processing requirements of the workpieces.
Longitudinal Grinding Method

The high speed rotation of the external cylindrical grinding wheel plays a grinding role, and the workpiece rotates in a rotary feed motion, and together with the worktable, it perform a longitudinal reciprocating linear feed motion.
When the worktable reciprocates one time, the grinding wheel completes a lateral feed along the grinding depth direction, and each feed( cutting depth) is very small.
All grinding allowance is completed in multiple reciprocating strokes.
Features of Longitudinal Grinding Method:
The working condition of the abrasive particles varies across the entire width of the cylindrical grinding wheel.
The grinding amount of the two sharp corners of the grinding wheel is relatively small, while the abrasive particles on the width of the grinding wheel are responsible for reducing the roughness value of the working surface. The grinding force is lower and the grinding heat is smaller for the longitudinal grinding method. It is used for precision grinding and can achieve smaller surface roughness and higher machining accuracy.
Because of small depth of cut and long reciprocating time of the worktable, the production efficiency is relatively low.
Cutting-in Grinding Method
Cutting- in grinding method, also known as lateral grinding method.
When the width of the cylindrical grinding wheel is more than the length of the external cylindrical of the workpiece, the grinding wheel can continuously cut into and grind horizontally, removing all machining allowances.
There is no longitudinal feed motion during grinding. During rough grinding, a higher cutting speed can be used, but the grinding wheel pressure is not easily too high.

During precision grinding, the cutting speed should be low to prevent workpiece burns and thermal deformation.
Features of the Cutting-in Grinding Method:
The working condition of the abrasive grains on the entire width of the grinding wheel is the same, fully utilizing the grinding effect of all abrasive grains. At the same time, with the continuous transverse feed, the basic grinding time is shortened, resulting in higher production efficiency.
When grinding, there is significant grinding force and heat, which can cause deformation and burns of the workpiece
Due to the lack of longitudinal feed motion, the surface morphology of the grinding wheel (dressing marks) will be copied onto the surface of the workpiece, affecting the surface roughness of the workpiece.
The cutting-in method is limited by the width of the external cylindrical grinding wheel and is only suitable for grinding external cylindrical surfaces with shorter length.
Segmented Grinding Method
This grinding method, also known as comprehensive grinding method, is a comprehensive application of the cutting-in method and the longitudinal method.

Firstly it used for rough grinding for the workpiece in sections with cutting-in grinding method, leaving a margin of 0.03-0.04mm, and then fine grinding to the size of the workpiece with the longitudinal method.
This method takes advantage of the high production efficiency of the cutting-in method and the high machining accuracy of the longitudinal method. When segmented grinding, there should be a 5-15mm overlap between adjacent sections.
This grinding method is suitable for the workpiece with large grinding allowance and good stiffness, and the length of the workpiece should also be appropriate..
Deep Grinding Method
When grinding, a smaller unidirectional longitudinal feed is used, and the longitudinal feed direction of the grinding wheel should face the head frame and lock the tailstock sleeve to prevent the workpiece from falling off. The hardness of the grinding wheel should be moderate and have good grinding performance.
Suitable for grinding workpieces with good rigidity.The grinder should have a high power stiffness.When grinding, a smaller unidirectional longitudinal feed is used, and the longitudinal feed direction of the grinding wheel should face the head frame and lock the tailstock sleeve to prevent the workpiece from falling off. The hardness of the grinding wheel should be moderate and have good grinding performance.

In mechanical processing, the measurement of product is one of the indispensable technology. The same goes for external cylindrical grinding. After external cylindrical grinding, measure the dimensional accuracy, roundness, and cylindricity. At the same time, any defects during measurement should be eliminated.
External cylindrical grinding wheels include ordinary abrasives, diamond abrasives, and CBN abrasives. Commonly used shapes include 1A1, 14A1, etc.
Related Products


Performance comparison of 5 Types Grinding Wheels
Type of Binder | Self-Sharpening | Sharpness | Life | Dressing Difficulty | Price |
Metal | 3/5 | 3/5 | 3/5 | 5/5 | 4/5 |
Resin | 5/5 | 4.5/5 | 3/5 | 1/5 | 2.5/5 |
Vitrified | 5/5 | 5/5 | 4/5 | 1/5 | 4/5 |
Electroplated | 4.5/5 | 5/5 | 3/5 | 0.5/5 | 4/5 |
Metal-Resin | 4/5 | 4.5/5 | 5/5 | 3/5 | 5/5 |
Diamond VS CBN Grinding Wheels

INQUIRY
Please Feel free to give your inquiry in the form below. We will reply you in 24 hours.