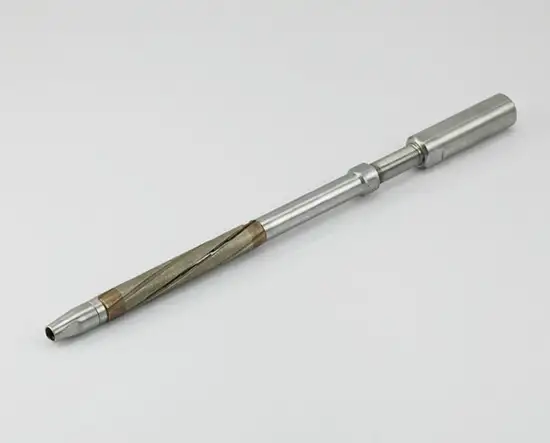
Single pass honing is a new process that combines ordinary honing with conventional reaming. It is a micron-level precision machining process that can process through holes, blind holes, keyway holes, step holes and other hole types.
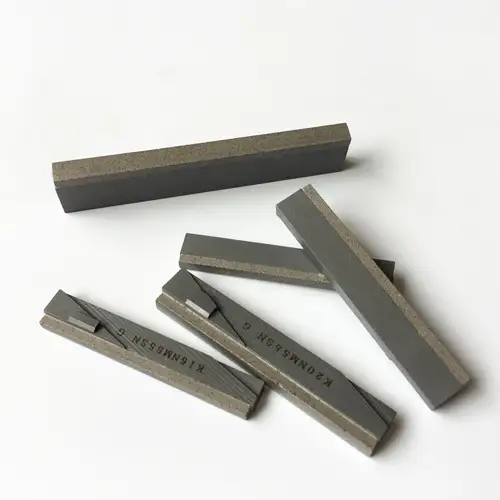
Single pass honing tools is a kind of combination of diamond stones and a reamer. It consists of honing mandrel and diamond abrasive sleeve(electroplated or sintered), which can be adjusted to compensate for the wear of diamond abrasive particles. It can be honed once and then exited by low-speed honing.
Application of Single pass honing tools:
Materials to be processed: castings, steel parts, quench-hardened parts, copper aluminum parts, ceramic parts, etc.
Hole types: through holes, blind holes, keyway holes, step holes
Application industries: automotive components, engine connecting rods, tappets, turbocharger housings, pistons, refrigerator compressor components, hydraulic valve sleeves, motor stators, etc.
Grinding workpiece
Structure of Single Pass Honing Tools
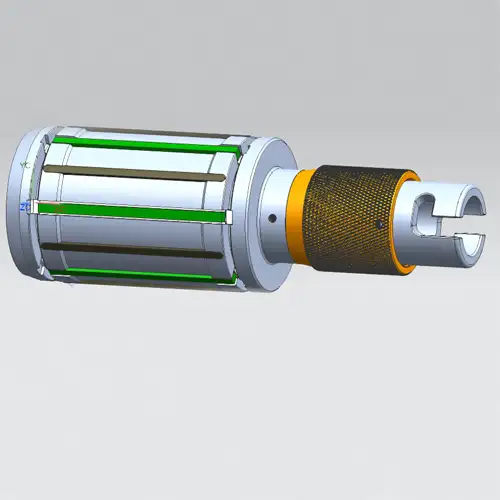
There are two types of single pass honing tools:fixed and adjustable. The honing sleeves include electroplated and metal sintered type. The abrasive mainly adopts diamond abrasive, and some uses CBN abrasive.
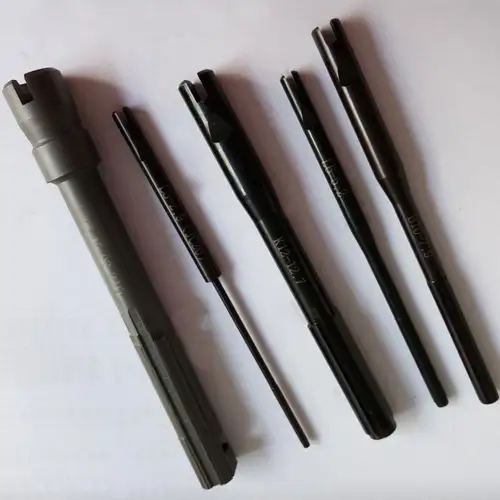
For example structure of electroplated adjustable single pass honing tools:The front end of reamer rod is designed with external threads, and the middle part of the rod is an external conical surface.
The conical surface is electroplated with diamond abrasive, which plays a role in adhesion with the inner conical surface of the hinge honing sleeve. The straight handle part of the rear end of the tool holder is connected to the machine shaft or floating connector.
The hinge honing sleeve has a through slot opening, and the inner hole is a combination of the inner conical surface and the outer conical surface of the tool holder.
The honing sleeve is electroplated with diamond grains of different grain sizes as needed, and the tool holder is equipped with several spiral slots that can remove chips.
The tool sleeve is installed on the hinge rod, and the adjusting nuts are installed on the external thread at the front end of the tool rod. Push the tool sleeve to move towards the larger end of conical surface by adjusting nut at the front end, thereby expanding the tool sleeve to process the workpieces.
Features of Single Pass Honing Tools
Electroplated bonding, good diamond bonding, uniform distribution of diamond grains, and high appearance quality.
The outer roundness of the front and rear guide of diamond reamer is 0.005mm, the cylindricity of that is 0.005mm/100mm. The cylindrical roughness of the front guide is Ra 0.63 micron, and that of rear guide is Ra0.16μm. The coaxiality between the handle and the front and rear guide parts is 0.015mm. The cylindricity of the workpiece being reamed is less than 0.003, the roughness is Ra 0.4-0.2, high precision, high efficiency, and long service life.
Instructions of Single pass honing tools
Selection of The Structure
Single pass honing tool is suitable for reaming black metals such as cast iron, ductile iron, quenched steel, and 45# steel. There are fixed diamond reamer and adjustable diamond reamer. The two structures of reamer can be used together in order to extent the life of reamer. Adjustable diamond reamer is used for rough and semi-finish reaming, and the fixed diamond reamer is used for finish reaming.
Selection of Reasonable Machining Allowance
It should not exceed 1/3-1/4 of the diamond abrasive size itself, otherwise the diamond reamer may get stuck in the workiece hole due to much chips, which will reduce the tool’s life.
For diamond honing reamer with grit of 80/100-100/120, the machining allowance will be controlled between 0.02mm-0.04mm.
For diamond honing reamer with grit of 170/200-230/270, the machining allowance will be controlled between 0.015mm-0.005mm.
For diamond honing reamer with grit of 325-400, the machining allowance will be controlled between 0.005mm-0.01mm.
Reciprocating Stroke Not Too Many Times In The Hole
Usually one reciprocating stroke is sufficient. At present, this kind of single diamond honing tool is used as grinding rod. Because increasing the reciprocating frequency too much will reduce the life of diamond reamer.
Selection of Reasonable Cutting Fluid
When honing cast iron holes, a mixture of 80% kerosene and 20% sulfurized oil or mechanical oil can be used as cutting fluid, or all kerosene can be used as cutting fluid. When processing steel parts, the mixture of 70% kerosene and 30% sulfurized oil can be used.
Reasonable Use The Tools
In order to improve the service life of diamond honing reamers, new reamers can be used for rough reaming. After honing 5000-6000 holes,they are changed to precision reamers to utilize the blunt abrasive particles to compress and polishing the workpieces. This not only reduces the surface roughness, but also increases the life of the reamer by more than twice.
Our single pass honing tools can be used on vertical honing machines from Sunnen, Engis, MAS, etc.
Related Products
Diamond Honing Sticks
CBN Honing Sticks
Honing Mandrel
Honing Head
INQUIRY
Please Feel free to give your inquiry in the form below. We will reply you in 24 hours.