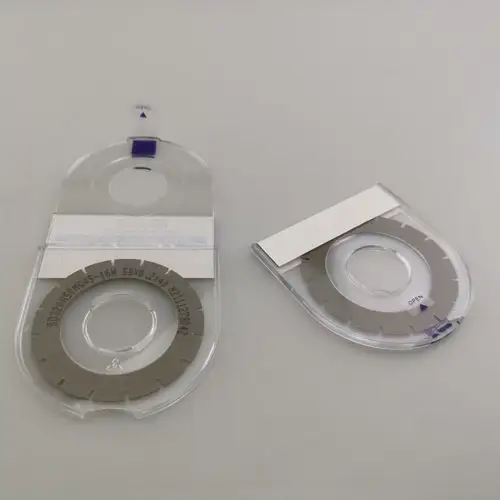
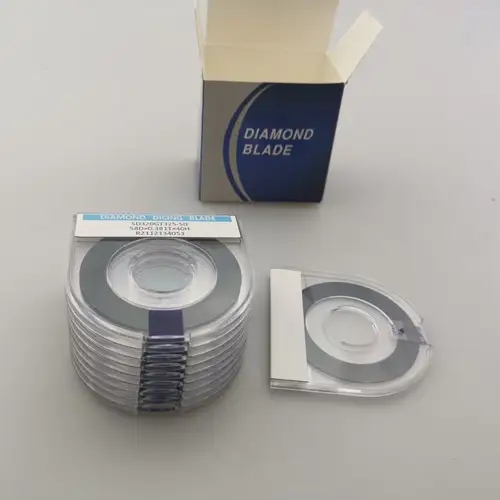
Newdiamondtool is a professional cutting, grinding, drilling and polishing system solution provider. Based on electroplated dicing blade, and sintered diamond balde, we also launched diamond dicing blade dress board that can adapt to various blades.
Dicing blade dressing board is mainly used for grinding electroplated & sintered diamond dicing blades, improving the cutting edge rate of diamond on the blade and achieving the concentric effect between the blade and the spindle.
Advantages of Diamond Dicing Blade Dressing Board
When pre dicing with dicing blade dressing board, it can be completed in short time and achieve good processing quality.
Using dicing blade dressing board for pre dicing can not only improve the cutting efficiency of the dicing blade, but also reduce the amount of tape and cooling water by reducing the pre dicing time.
Why Do We Need To Dress The Blade
Adjust The Roundness
When a new dicing blade in installed on the spindle and flange, although the blade is in direct contact with the top of the spindle, there is still a gap between the blade and spindle. The center of the blade is offset from the center of the spindle, which is the eccentricity of the blade. When rotating at high speed, it is not really circular.
If the dicing blade is used with eccentricity, only a part of the blade will work, and excessive load can easily cause reverse cutting and overload, affecting the product quality.
Influence of eccentricity on back edge chipping
The larger the eccentricity, the larger the size of back edge chipping when initial cutting.
After being dressed, the new dicing blade can adjust its roundness, reduce eccentricity and improve cutting quality.
The eccentricity of dicing blade is 0μm, and the back of product chips.
The eccentricity of dicing blade is 10μm, and the back of product chips.
The eccentricity of dicing blade is 15μm, and the back of product chips.
Cutting Edge
When using a new dicing blade, diamond is not fully exposed and the cutting ability is poor. Pre cutting can fully expose the diamond and create the chip flute, increasing chip removal capacity.
Diamond Dicing blade before dressing
Diamond Dicing blade after dressing
Create The Chip Flute To Increase Chip Removal Capacity.
When using a new dicing blade, diamond is not fully exposed and the cutting ability is poor. After dreesing, the diamond is fully exposed and can create the chip flute, increasing chip removal capacity.
Regularly clean the dirt on the blade to ensure smooth chip removal.
Parameters of the Dicing Blade Dressing Board
Selection of The Use of The Dicing Blade Dressing Plate
Dressing Situation Of Various Types Of Dicing Blades:
Resin bond diamond dicing blade: When the resin bond diamond dicing blade is first installed, it needs to be dressed to make the blade and spindle concentric. There is basically no need for dressing during cutting process.
Electroplated diamond dicing blade: The dicing blade has been pre dressed before leaving the factory. After installation, it mainly adjusts the eccentricity of dicing blade, wheel hub, and spindle, and rarely needs to be dressed in the later cutting process.
Metal bond diamond dicing blade: It is the main service object for dicing blade dressing board. When the blade initial installation, the blades need to be dressed to achieve the concentric. During the cutting process, due to the poor self sharpness of the metal bond agent, the blade is easily dull. The diamond can be re exposed by timely dressing, maintaining high sharpness, and the deposit on the blade can be removed at the same time.
Case Explanation
The customer used QFN dicing blades. The new dicing blades are sharpened by cutting the QFN frame after installation, without a dressing process. The initial cutting effect of the new dicing blades is not good. And it is recommended to add the resin bond dicing blade dressing process with dressing board, improving the overall cutting quality of the new dicing blades.
Workpiece Information:
Product: QFN Coating: Tin plated on the surface Material: Epoxy resin+copper Original blade information: 58 * 0.33 * 40-240#
Original Processing Requirements:
Burr size<50 μ m;
Edge chipping size<30 μ m;
Optimization Requirements:
Burr size<15 μ m;
Edge chipping size<8 μ m;
Selection of Various Parameters For Blade Dressing
Type of cutting board: Resin dressing board Grain size of the dressing board: 400# Dressing speed (rpm): 17000 Dressing feed rate (mm/s): 6 Dressing depth (mm): 0.5 Number of blade dressing: 5 Dressing time: 1 minute
Test Result
Burr size:<10 μ m
Edge chipping size:<5 μ m
After adjusting the process, the cutting quality of the dicing blade has been greatly improved, which meets the current production needs of the customer.
Related Products
Hubless Metal Bond Diamond Dicing Blade
Hubless Resin Diamond Dicing Blade
Diamond Dicing Blade
Electroplated Wafer Dicing Blade
INQUIRY
Please Feel free to give your inquiry in the form below. We will reply you in 24 hours.