5 Types of Diamond Tools for Grinding Thermal Spray Coating
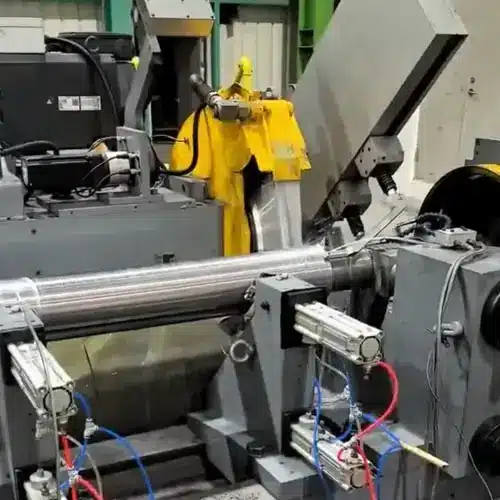

Diamond Tools for Grinding Thermal Spray Coating
- Resin bond diamond wheel
- Vitrified bond grinding wheel
- Diamond abrasive belt
- Diamond flap wheel
- Diamond honing stone
Thermal spraying has high hardness and workpieces have different shapes, so diamond tools need to be selected according to the shape of the workpiece.
The surface hardness of thermal spray coating is high, and diamond tools are ideal for grinding it. Common diamond tools for Grinding Thermal Spray Coating include diamond grinding wheel, diamond abrasive belt, diamond flap wheel, and etc.
Introduction of thermal Spray coating
Thermal spray coating is a kind of processing method for material surface that heat the sprayed materials to a molten state by various heat sources, atomizes them by airflow and sprays them onto the surface of the parts, forming the material surface with different functional spray coating layers.
The working principle of thermal spray coating usually comes from welding. According to the different heat sources, it divided into flame spraying, arc spraying, and plasma spraying. In the 1980s, flame spraying gave rise to high-speed flame spraying, also know as high-velocity oxygen-fuel spraying( HVOF).

There are a wide range of coating materials that can be sprayed, and thermal spraying technology can be used to spray almost all solid engineering materials, such as tungsten carbide, ceramic, metal, graphite, etc
Applications of thermal spray coating: Thermal spraying technology is now widely used in many industries such as aerospace, aviation, electronics, communication, semiconductor, automotive, power, machinery, artificial implantation, metallurgy, chemical, petroleum, coal, railway, kitchenware, textile, etc.
Choose Diamond Tools for Grinding Thermal Spray Coating
The surface roughness and coating uniformity of HVOF sprayed parts cannot meet the engineering requirements, and the surface of workpiece need to be ground by machine after spraying.
Grinding is the main method for processing thermal spray coating, which can improve the corrosion resistance of coatings. The surface roughness can be less than 0.2, achieving a mirror finish. There are diamond grinding wheel, diamond abrasive belt, diamond flap wheel and etc. for choosing.
Resin Bond Diamond Grinding Wheel For Thermal Spray Coating

Resin bond diamond grinding wheel can be used for grinding tungsten carbide of thermal spray coating with good grinding efficiency, and the spray coating can achieve good surface roughness. It is easy for dressing. It can be suitable for different spay coatings by adjusting the formula.
The entire process is usually divided into three stages: rough grinding, fine grinding, and finish grinding
When rough grinding, diamond grinding wheel has large diamond grains, which has good removal efficiency.
When fine grinding, considering the removal amount, the surface roughness of thermal spray coatings of the workpiece has achieved a good effect, or it can already meet the engineering requirements.
When finish grinding, achieve a high surface roughness of the coatings. Sometimes, fine grinding has already met the customers’ needs.

参数图
Vitrified Diamond Grinding Wheel for Thermal Spray Coating
Vitrified bond diamond grinding wheel can be used for cylindrical grinding the workpiece with thermal spray coatings such as steel based tungsten carbide.
When the width of the grinding wheel is more than the length of the external cylindrical of the workpiece, the grinding wheel can continuously cut into and grind horizontally, removing all machining allowances. There is no longitudinal feed motion during grinding. During rough grinding, a higher cutting speed can be used, but the grinding wheel pressure is not easily too high. During precision grinding, the cutting speed should be low to prevent workpiece burns and thermal deformation.


图标
Diamond Abrasive Belt for HVOF WC Coating

The surface quality the workpiece ground by diamond abrasive belt is high, mainly manifested in small surface roughness value, good residual stress state, and no micro cracks or changes in metallographic structure on the surface. From the perspective of surface roughness, it can currently reach Ra0.01mm, achieving the effect of mirror grinding. However, for surface roughness above Ra0.1mm, it is very easy to achieve.
There are resin bond and electroplated diamond abrasive belt. Electroplated diamond abrasive belt has higher grinding efficiency. Resin diamond sand belt has better life and surface roughness.In addition, diamond abrasive belt has different patterns on the surface, some of which are gentle during grinding, while others are aggressive.

Diamond Abrasive Belt vs Diamond Grinding Wheel
Diamond abrasive belt does not require dressing. Because it belongs to non-contact grinding, the accuracy of machining cylindricity is lowder than that of diamond grinding wheel. If contact wheel grinding( contact wheel hardness of 90) is used, it can reduce the processing time and can achieve the machining accuracy requirements of the workpiece.
Grit: 40#-5000#
Size: Width:5mm-350mm, Length: 150mm-5000mm
Diamond Flap Wheel for Thermal Spray Coating
Diamond flap disc and diamond flap wheel are mainly used for grinding and polishing flat, curved, and complex surface, which mainly used on the hand-held grinders, pneumatic and electric grinder with speed of 10000-2000rpm.
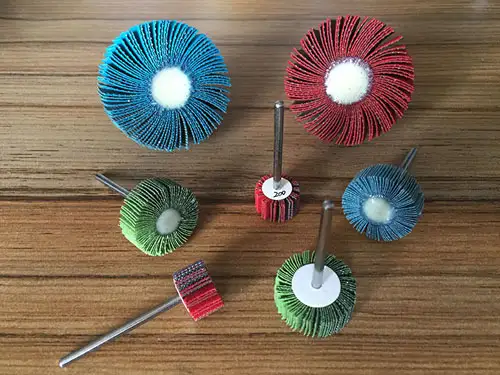
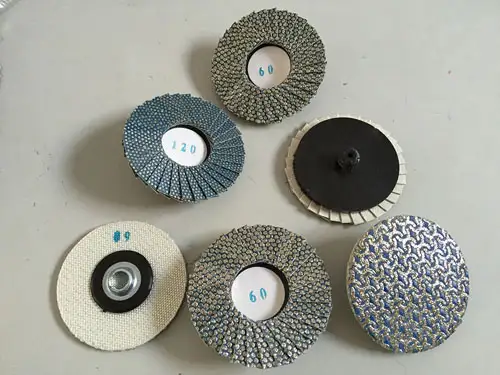
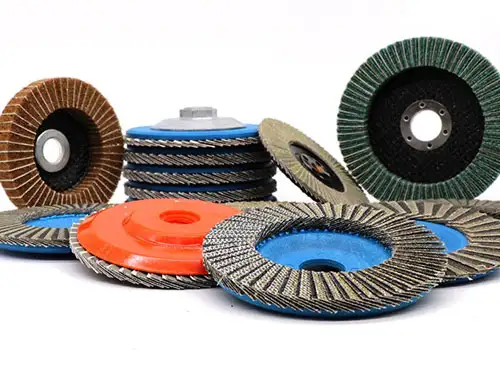
Features: flexible structural design, sharp grinding
Diamond Honing Stone for Thermal Spray Coatings in Cylinder
After thermal spraying treatment on the surface of engine cylinders and piston rings, form the special wear-resistant layer which can improve wear resistance, reduce friction coefficient by 20%-30%, and reduce fuel consumption.
For example, the process flow of plasma spraying is:
Cylinder bore fine boring – cylinder bore roughening – cleaning – cylinder bore spraying – overspray treatment – final honing.

The cylinder holes after thermal spraying still need to be honed to meet the requirements of product use. Regarding the coating material and the shape of coating surface, there are small wave shapes on the coating surface. When the coating thickness is controlled within 0.55 mm, thermal spraying will not affect the positional accuracy of the honed cylinder hole. The floating honing process same as that of current cast iron cylinder liner can meet the honing requirements. The difference is that it need to optimize the grain size and material of diamond honing stones and adjust the relevant honing parameters to ensure the honing requirements of thermal spray coating.
According to the size, material, surface roughness requirements of thermal spray coating workpiece, choose the suitable diamond tools for grinding.
Related Products


Performance comparison of diamond grinding wheels with various binders
Type of Binder | Self-Sharpening | Sharpness | Life | Dressing Difficulty | Price |
Metal | 3/5 | 3/5 | 3/5 | 5/5 | 4/5 |
Resin | 5/5 | 4.5/5 | 3/5 | 1/5 | 2.5/5 |
Vitrified | 5/5 | 5/5 | 4/5 | 1/5 | 4/5 |
Electroplated | 4.5/5 | 5/5 | 3/5 | 0.5/5 | 4/5 |
Metal-Resin | 4/5 | 4.5/5 | 5/5 | 3/5 | 5/5 |
INQUIRY
Please Feel free to give your inquiry in the form below. We will reply you in 24 hours.